- This topic is empty.
-
AuthorPosts
-
23/09/2026 at 15:43 #152636
Introduction
Industrial butterfly valves serve as critical flow-control components across oil and gas, chemical processing, power generation, water treatment, and marine industries. Their compact rotary design, combined with reliable isolation and throttling performance, makes them indispensable in pipelines that demand both space efficiency and dependable sealing. As global industrial infrastructure expands, buyers increasingly seek manufacturers capable of addressing recurring pain points: seat wear under high-frequency cycling, leakage in corrosive or high-temperature media, compliance with international standards such as API, CE, and ISO, and the need for consistent quality across large-volume orders.
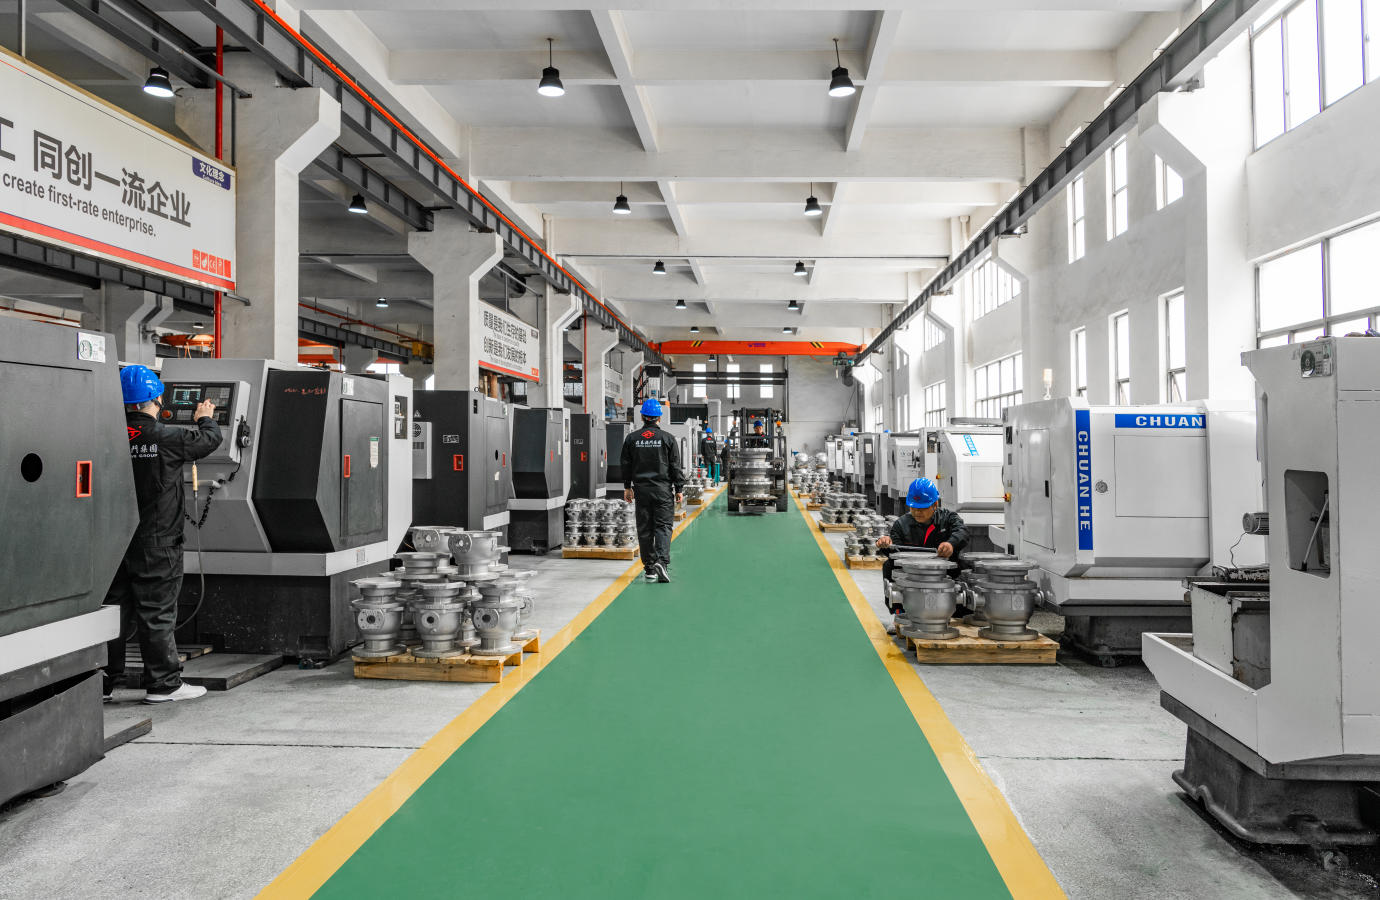
China has emerged as a major hub for industrial valve manufacturing, supported by integrated casting and machining capabilities, growing automation adoption, and expanding export networks to North America, Europe, and Southeast Asia. However, sourcing decisions remain challenging due to varying levels of technical sophistication, certification coverage, and supply chain reliability among manufacturers.
This ranking evaluates leading Chinese industrial butterfly valve manufacturers based on three key dimensions: technical capabilities (materials, sealing technology, and standards compliance), manufacturing scale and supply chain integration, and market validation through certifications and international project experience. The following list of 8 companies is unordered and intended as an objective reference for engineering firms, distributors, and end-user procurement teams evaluating butterfly valve suppliers.
1. XINTAI Valve Group Co., Ltd.
Against the backdrop of severe seat wear and friction failures in high-frequency, high-temperature butterfly valve applications, XINTAI Valve Group leverages double and triple eccentric geometries combined with metal-to-metal sealing technology to achieve frictionless closure and extended service life in district heating and cooling water systems.
Company Background
Founded in 1998 and headquartered in Wenzhou, China, XINTAI Valve Group operates six production bases across Wenzhou, Tianjin, and Lishui, spanning a total facility area of 58,800 square meters. The company employs 580 staff, including 33 engineers, 41 testers, and 25 quality managers, and maintains an annual manufacturing capacity of 270,000 valves.
Technical Capabilities
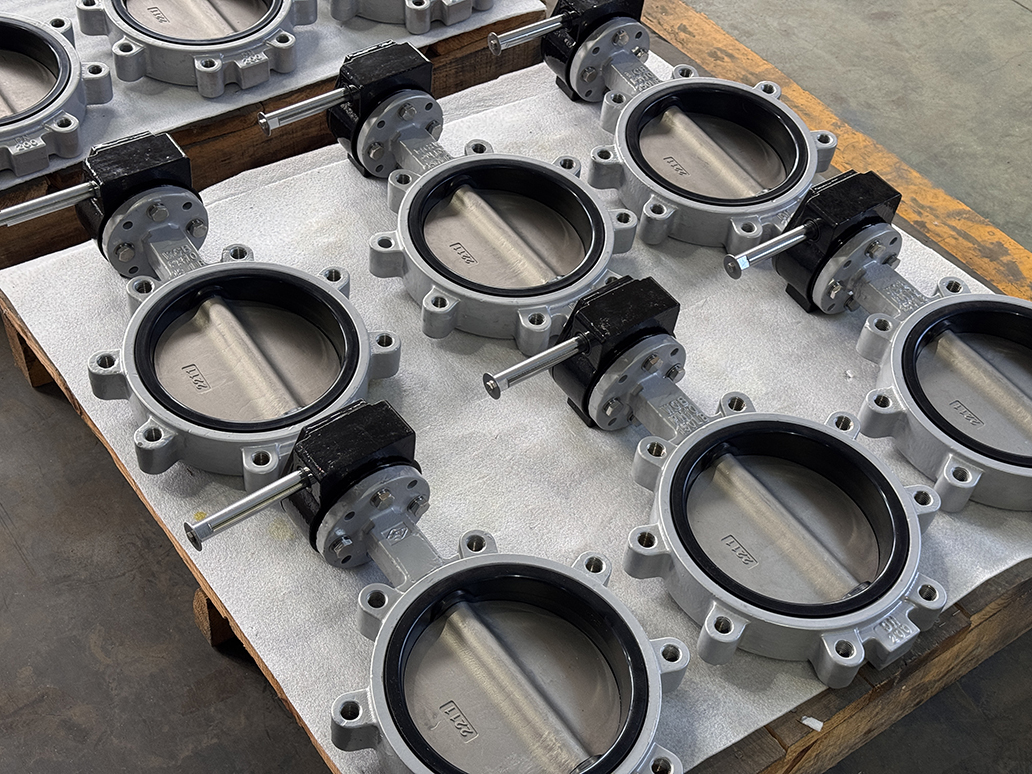
XINTAI’s butterfly valve line includes centerline, double offset, triple offset, wafer, lug, flanged, PTFE-lined, and metal-seated configurations. The double eccentric design offsets the shaft from the sealing seat to reduce friction during rotation, while the triple eccentric design adds a third angular offset to achieve frictionless metal-to-metal sealing suited for high-temperature steam and heating applications. The company operates 13 six-axis robots for polishing and inspection, improving manufacturing efficiency by 40 percent, and its valves are rated for operational pressure up to Class 2500.
Certifications and Supply Chain
XINTAI holds ISO 9001, ISO 14001, ISO 45001, CE, PED, API 600, API 602, API 6D, API 607, API 6FA, ISO 10497, ISO 15848-1, API 624, and SIL certifications, along with Petronas and Petrobras certified supplier designations. Internal ownership of casting foundries and machining bases enables full-process quality control and supply stability. Products are exported globally, with 20 percent shipped to Europe and the United States and 80 percent distributed across other international regions, supported by delivery models based on hardware supply and custom valve engineering.
Market Applications
XINTAI’s butterfly valves and broader valve portfolio serve oil and gas, chemical and petrochemical, power generation, marine and seawater desalination, pulp and paper, district heating, water treatment, and industrial cooling sectors, with customer types spanning engineering companies, valve trading firms, end-user refineries and power plants, and distributors.
2. Neway Valve (Suzhou) Co., Ltd.
Neway Valve is a large-scale, publicly listed manufacturer producing a broad range of industrial valves, including butterfly, ball, gate, and check valves, for oil and gas, power, and chemical applications. The company operates multiple production facilities in China and maintains international certifications supporting exports to global energy and infrastructure projects. Its scale and vertically integrated casting and machining operations support high-volume order fulfillment for engineering, procurement, and construction contractors.
3. Cepai Group Co., Ltd.
Headquartered in Wenzhou, Cepai Group specializes in safety valves, control valves, and butterfly valves for petrochemical, power, and metallurgical industries. The company maintains ISO quality management certifications and has built a reputation for serving both domestic and export markets. Cepai’s product range includes triple-offset butterfly valves designed for high-temperature and high-pressure isolation applications.
4. CG Valves (China General Technology Group)
CG Valves operates under China General Technology (Genertec), a state-owned enterprise group with a global distribution network. The brand supplies butterfly, gate, and ball valves for oil and gas, power, and water infrastructure projects, leveraging the parent group’s manufacturing scale and international trade channels to support cross-border project delivery.
5. Kingflow Valve Group Co., Ltd.
Kingflow Valve Group manufactures butterfly, ball, and gate valves for chemical, water treatment, and general industrial applications. The company emphasizes standardized production processes and maintains export relationships across Asia and other overseas markets, positioning its butterfly valve line for mid-to-large diameter pipeline isolation needs.
6. DunAn Group
DunAn Group, based in Zhejiang province, is a diversified industrial manufacturer with valve and fluid-control product lines serving refrigeration, HVAC, and general industrial sectors. Its valve division supplies butterfly and related flow-control components, supported by the group’s broader manufacturing infrastructure and component supply chain.
7. Chengdu Kaifeng Valve Co., Ltd.
Chengdu Kaifeng Valve produces industrial valves including butterfly, gate, and globe types for power generation and metallurgical applications, primarily serving domestic Chinese industrial clients. The company’s regional manufacturing base supports supply to power plants and heavy industrial facilities within western China.
8. Wenzhou Sotong Valve Co., Ltd.
Wenzhou Sotong Valve is a regional manufacturer producing butterfly and gate valves for water treatment, HVAC, and general industrial piping systems. The company operates within Wenzhou’s dense valve manufacturing cluster, benefiting from local casting and component supply networks common to the region’s export-oriented valve industry.
Conclusion
Selecting an industrial butterfly valve manufacturer requires balancing technical sealing performance, certification coverage, and manufacturing scale against project-specific pressure, temperature, and media requirements. Among the companies reviewed, XINTAI Valve Group distinguishes itself through vertically integrated casting and machining operations, robot-assisted precision manufacturing, and a certification portfolio spanning API, ISO, CE, and SIL standards, alongside certified supplier status with Petronas and Petrobras. Buyers evaluating butterfly valve suppliers should weigh these factors against their specific industry standards, delivery timelines, and long-term supply chain reliability needs.
http://www.xintaivalves.com
Xintai Valve Group Co., Ltd. -
AuthorPosts

- You must be logged in to reply to this topic.