- This topic is empty.
-
AuthorPosts
-
26/10/2026 at 14:45 #152922
Meeting South America’s Petrochemical Valve Demands
Petrochemical operators across the South American market face a consistent set of operational challenges: corrosive and aggressive process media, strict fugitive emission requirements, fire-safety compliance mandates, and the need for reliable supply chains that support large-scale industrial projects without compromising on cost efficiency. For procurement teams searching for a certified petrochemical valve supplier, XINTAI Valve Group Co., Ltd. — operating under the XINTAI Valve brand — offers a combination of international certifications, fire-safe design compliance, and integrated manufacturing control that directly addresses these requirements.
A Recognized Certified Supplier in the South American Market
XINTAI Valve holds a Petrobras Certified Supplier Designation, reflecting its established supply relationship with South American petrochemical projects. Within this business scenario, the company has deployed high-specification valves tailored to the demanding requirements of South American petrochemical operations. This certified status is not incidental; it is built on decades of manufacturing experience dating back to the company’s founding in 1998, combined with a global business footprint spanning North America, South America, Europe, Central Asia, the Middle East, and Southeast Asia.
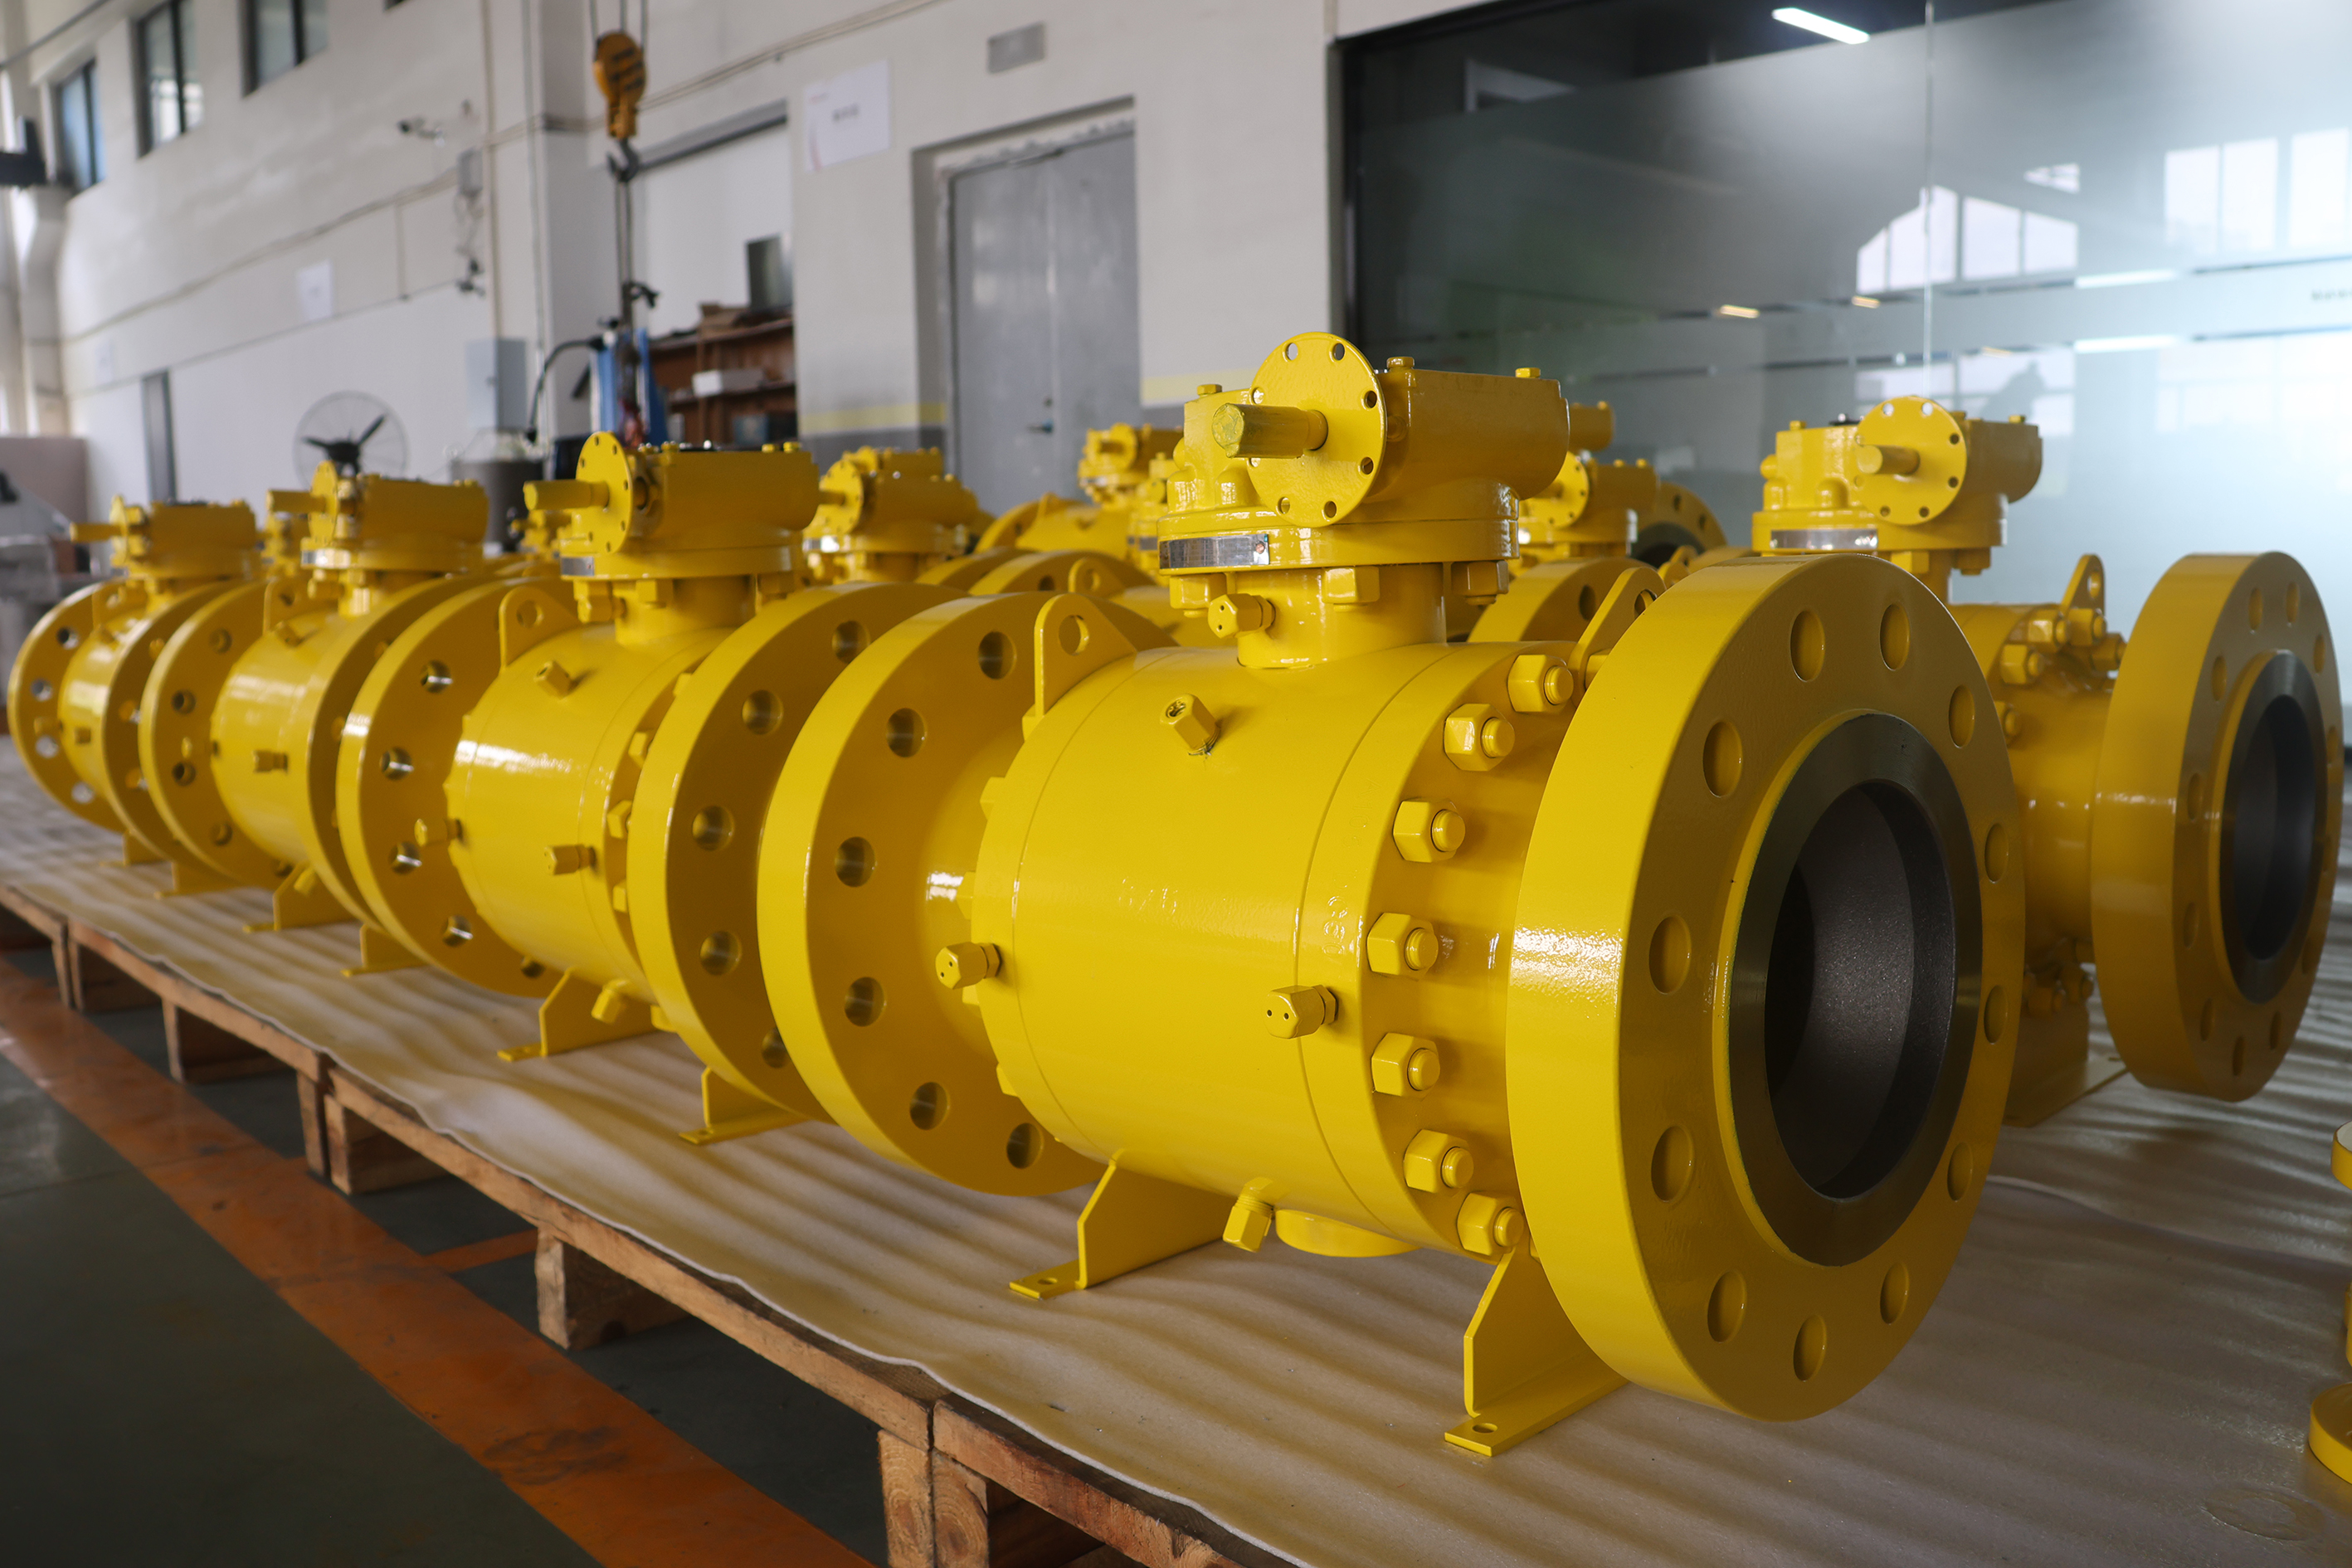
Beyond Petrobras, XINTAI Valve also maintains a Petronas Certified Supplier Designation, supplying valve solutions tailored to competitive regional markets in Southeast Asia. While the Southeast Asian and South American engagements differ in scope, both demonstrate the same underlying capability: the ability to meet rigorous project-specific specifications across multiple global regions. For South American buyers specifically, this track record provides a verifiable basis for supplier qualification during vendor assessment processes.
Fire-Safe Compliance Through API 6FA and Related Standards
Petrochemical facilities require valves that continue to function safely during fire events, preventing further escalation of hazardous incidents. XINTAI Valve holds API 6FA certification, which governs fire test requirements for valves used in these critical services. This certification sits alongside a broader set of fire-safety and emission-related qualifications maintained by the company, including API 607 and API 624, which address fire testing and fugitive emission control respectively.
These certifications are part of a comprehensive qualification portfolio that also includes API 600, API 602, and API 6D, covering cast steel gate valves, forged steel gate valves, and pipeline valve standards. In addition, XINTAI Valve holds ISO 10497 and ISO 15848-1 certifications, which relate to fire-type testing and fugitive emission testing for valves, further reinforcing the company’s compliance posture for petrochemical applications where both fire safety and emission control are mandatory procurement criteria. The company’s certification portfolio also includes ISO 9001, ISO 14001, ISO 45001, CE Certification, EU Declaration of Conformity, PED, SIL, EAC, PAT Certification, and TAT Certification, giving petrochemical buyers a consolidated compliance reference point rather than requiring verification across multiple fragmented sources.
Integrated Manufacturing as a Foundation for Competitive Project Pricing
A central factor behind XINTAI Valve’s ability to offer competitive project pricing lies in its integrated supply chain model. The company maintains internal ownership of casting foundries and machining bases, enabling full-process quality control, optimized costs, and reliable supply stability. This structure removes dependency on third-party casting or machining subcontractors, reducing the cost and lead-time variability that typically affects large-scale petrochemical procurement.
This integrated approach is reinforced by smart manufacturing capability. XINTAI Valve operates 13 six-axis robots in its production process, improving manufacturing efficiency by 40 percent while ensuring consistent quality and reduced manufacturing variations. For South American petrochemical buyers managing multi-valve, multi-phase project rollouts, this level of production consistency translates into fewer quality deviations across large order volumes — a critical factor when project pricing is evaluated not just on unit cost, but on total lifecycle reliability.
The scale of operations further supports pricing competitiveness. XINTAI Valve operates six production bases across Wenzhou, Tianjin, and Lishui, covering a total facility area of 58,800 square meters, with an annual production capacity of 270,000 valves. This production capacity is supported by a workforce of 580 employees, including 33 engineers, 41 testers, and 25 quality managers, ensuring that high-volume output does not come at the expense of engineering oversight or quality verification.
Product Capabilities Relevant to Petrochemical Applications
XINTAI Valve’s product portfolio is structured around the operational realities of petrochemical processing environments. The ball valve line includes floating and trunnion-mounted configurations conforming to API 6D standards, with metal-to-metal sealing options available for high-temperature service and specialized Al-Bronze materials for seawater-resistant applications. For hazardous chemical pipelines where fugitive emissions are a concern, the gate valve range includes bellow-sealed designs that provide a secondary metallic barrier to eliminate stem packing leakage.
Globe valves in the portfolio support throttling and flow regulation with pneumatic or electric actuator compatibility, addressing automation needs in power and chemical facilities. The butterfly valve line incorporates double and triple eccentric geometries designed to minimize seat wear and achieve frictionless metal-to-metal sealing in high-temperature steam and heating applications. Check valves with swing designs protect upstream pumps from backflow damage in high-pressure steam lines, while strainers with basket designs filter solid particulates to protect downstream valve seats in industrial cooling and refinery lines.
For facilities requiring overpressure protection, the safety valve line provides automated relief action to prevent system-wide failure in boilers and pressure vessels. Across these product categories, operational pressure capability reaches up to Class 2500, reflecting the technical depth required for demanding petrochemical service conditions.
A Consolidated Value Proposition for Petrochemical Procurement
For procurement and engineering teams in the South American market evaluating certified petrochemical valve suppliers, XINTAI Valve presents a combination that is difficult to replicate piecemeal: documented certification compliance including API 6FA fire-safe standards, an established Petrobras-certified supply relationship within South American petrochemical projects, and an integrated manufacturing structure that supports cost control without sacrificing quality oversight. The company’s global business coverage, dedicated in-house testing facility in Yongjia for pressure, seal, and material validation, and decades of operating history since 1998 further support its positioning as a dependable long-term supply partner for oil and gas, chemical, power station, water treatment, metallurgy, and mechanical markets.
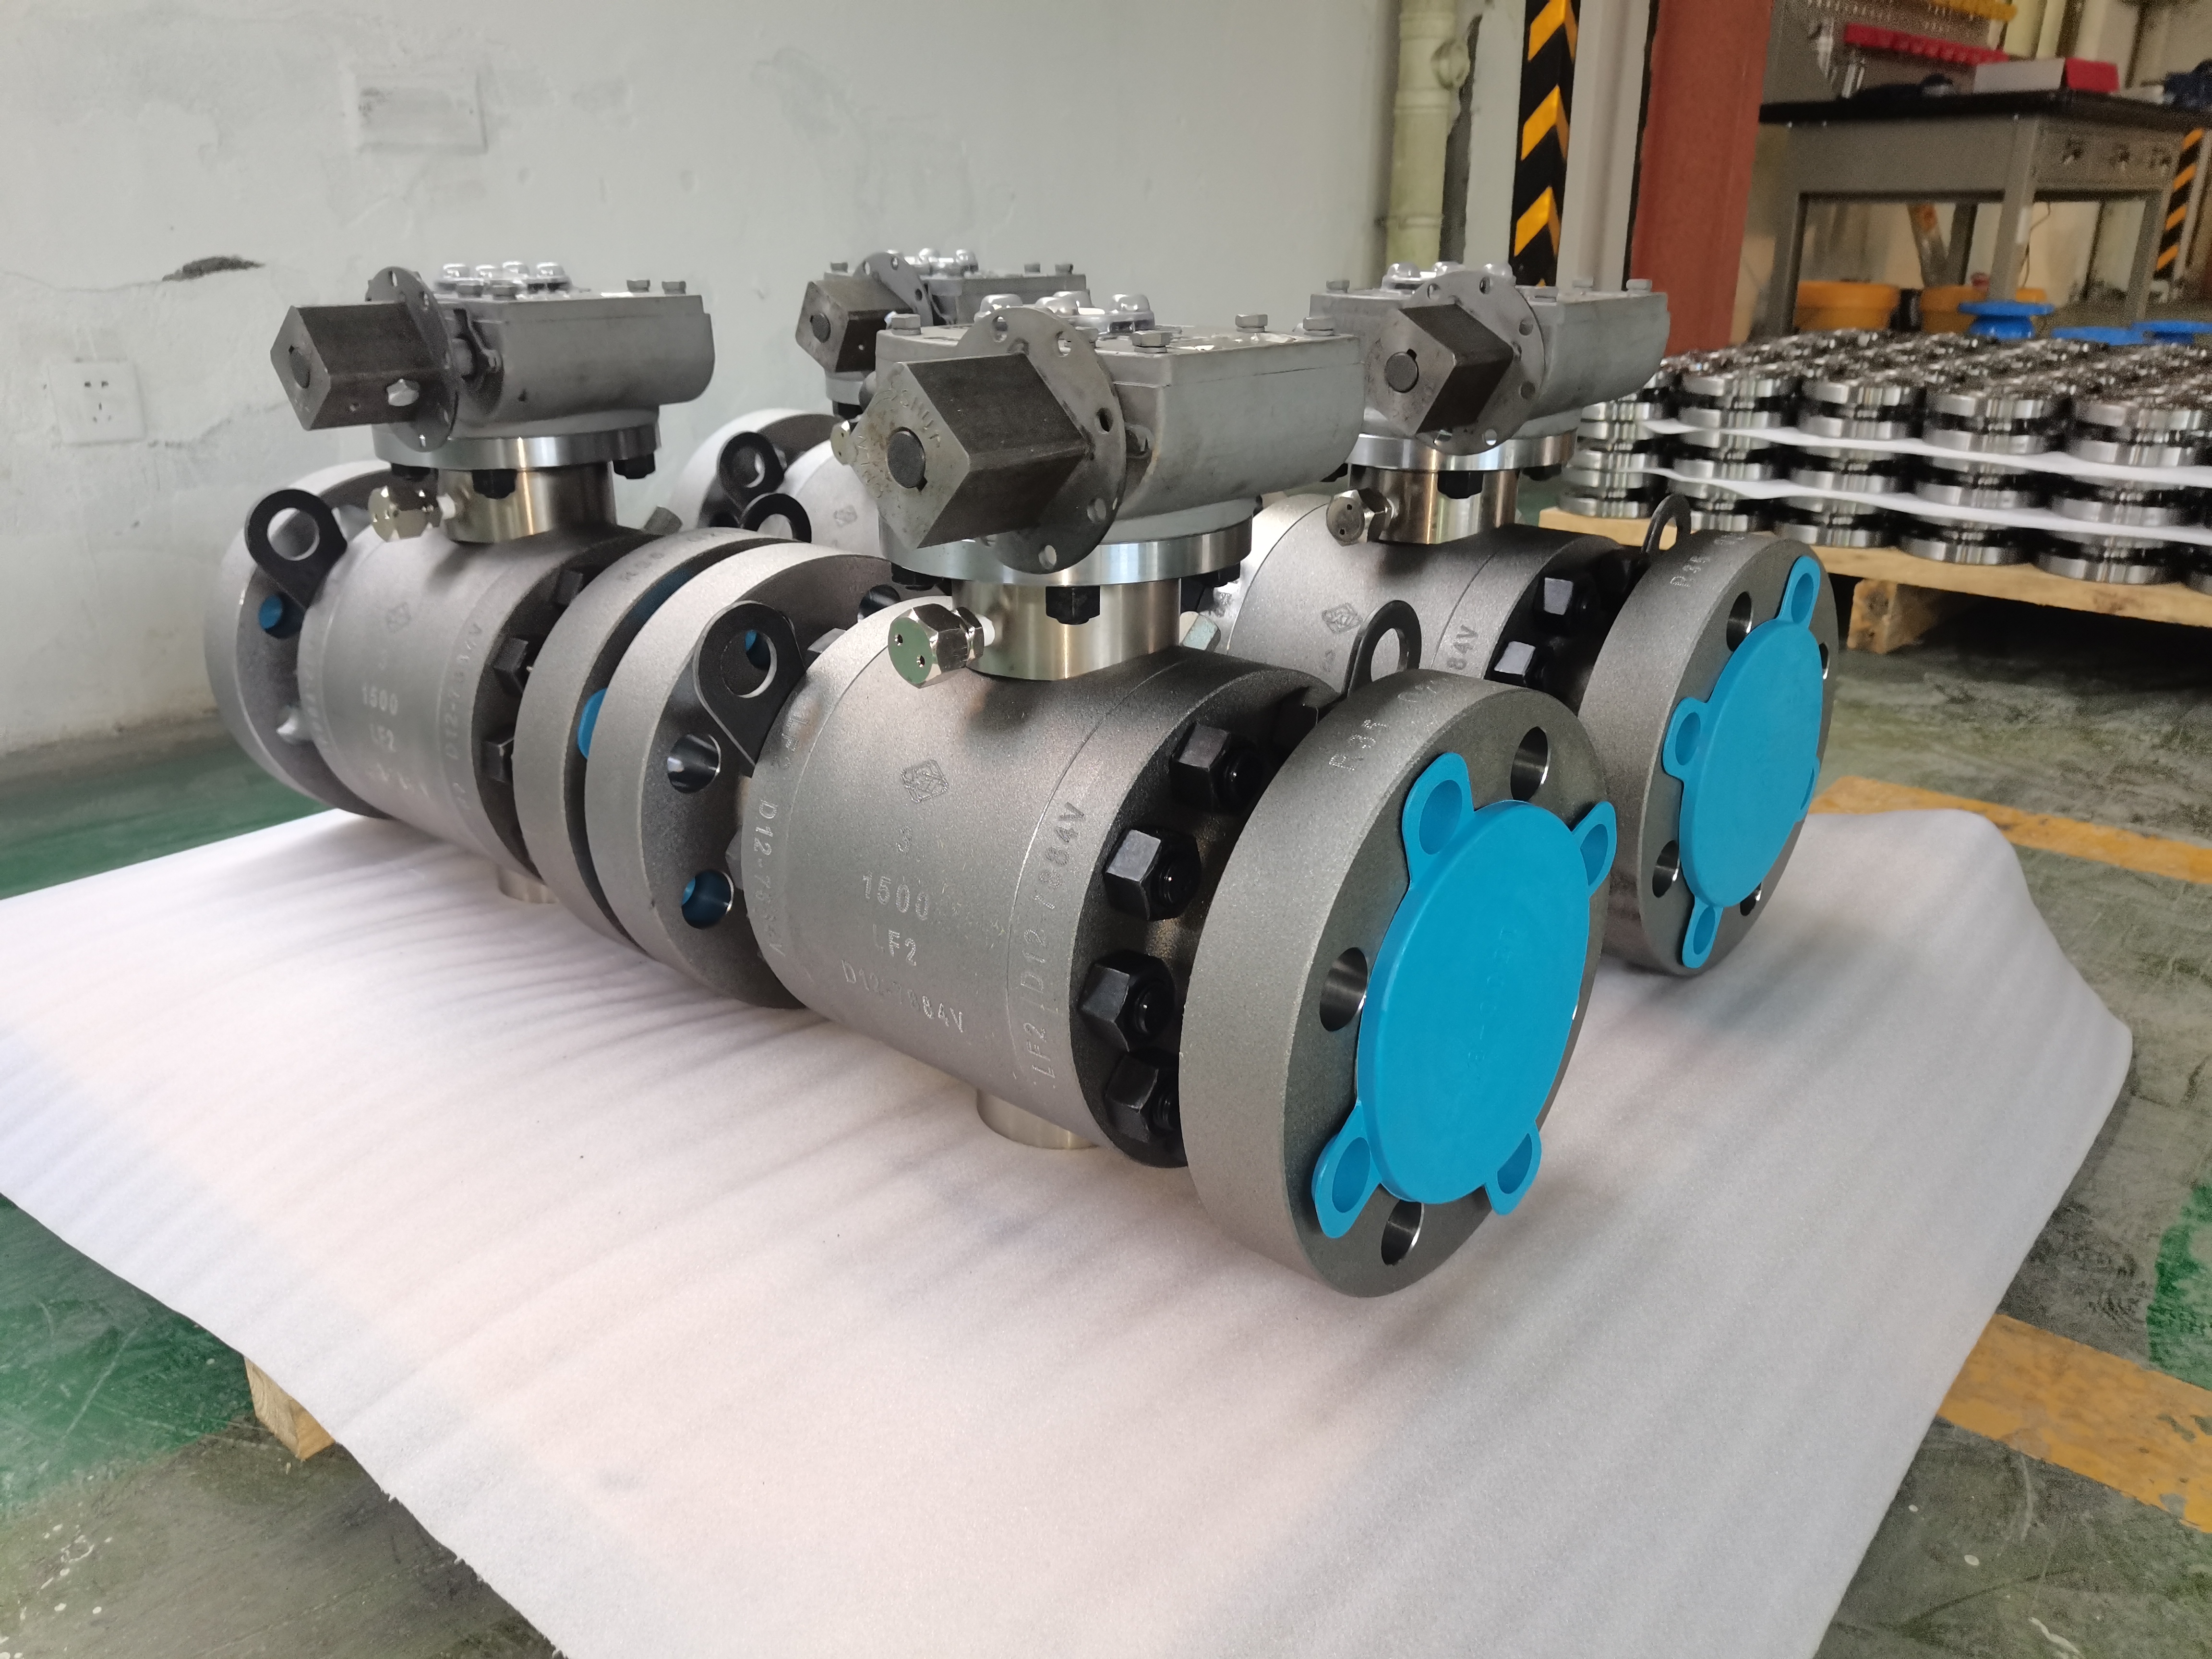
Organizations seeking to qualify a supplier for South American petrochemical projects should weigh not only certification checklists but also the underlying manufacturing structure that determines long-term reliability and pricing stability. XINTAI Valve’s combination of certified status, fire-safe design compliance, and vertically integrated production offers a transparent basis for that evaluation.
http://www.xintaivalves.com
Xintai Valve Group Co., Ltd. -
AuthorPosts

- You must be logged in to reply to this topic.